 EN
A Complete Industrial Guide
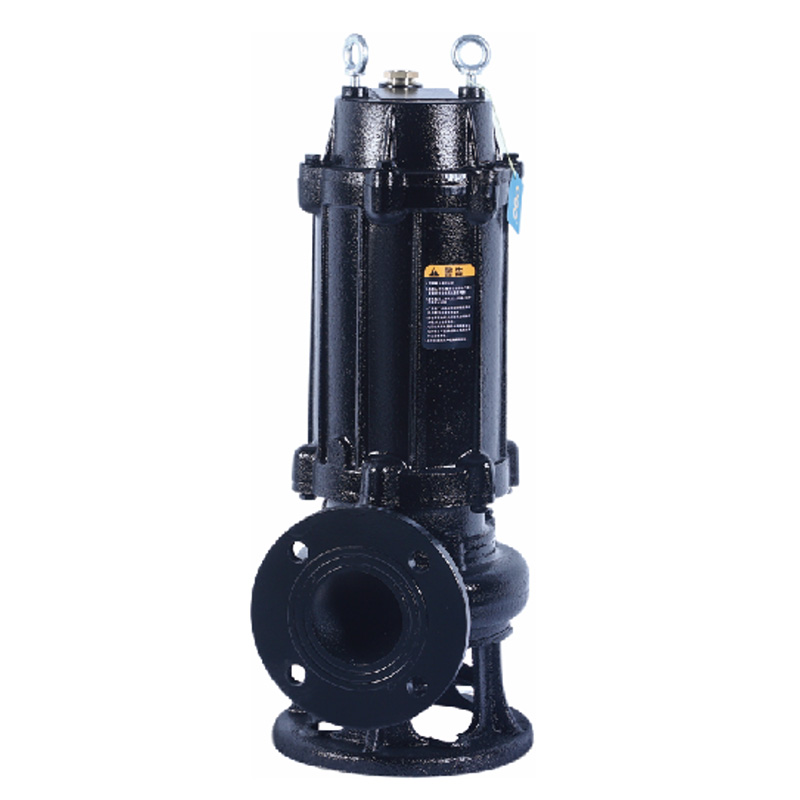
Submersible pumps stand out as one of the most reliable engineering solutions for moving liquids efficiently and safely across a wide spectrum of modern industrial, commercial, and residential applications. Unlike traditional surface-mounted pumps that constantly struggle with suction lifts, cavitation risks, and troublesome priming headaches, a submersible pump operates entirely below the liquid surface. By pushing fluid upward directly from the source rather than pulling it through an extended vacuum line, these specialized units minimize mechanical stress, reduce energy consumption, and deliver exceptionally high performance across diverse and demanding environments.
Whether dealing with accumulated rainwater in a deep excavation pit, extracting clean groundwater from a deep borehole, managing large-scale agricultural irrigation systems, or handling heavy municipal sewage, choosing the right machinery depends entirely on matching the pump design to your specific operating conditions. Sourcing reliable equipment from trusted manufacturers like Flyaway ensures that your pumping systems meet rigorous international standards for durability, hydraulic efficiency, and fluid dynamics. Modern infrastructure projects across the globe increasingly rely on these submerged configurations because they offer superior energy efficiency, quieter operation, and significantly lower long-term maintenance overhead compared to traditional above-ground alternatives.
Drainage and Dewatering Applications
Unwanted water accumulation can halt construction projects, flood commercial basements, and damage critical utility vaults in a matter of hours. Submersible drainage pumps provide a fast, highly effective way to clear flooded areas, control groundwater seepage, and keep excavation sites dry during heavy precipitation events.
When dealing with relatively clean water or minor debris, these robust units rapidly transfer liquid away from collection points to approved municipal drainage locations. However, site conditions dictate operational success. If the water contains abrasive sand, heavy silt, or construction grit, standard clean-water models will experience premature mechanical wear and frequent clogging. Selecting heavy-duty drainage units engineered by Flyaway guarantees robust impeller designs, high-grade motor housings, and abrasion-resistant materials capable of handling challenging particulate loads without unexpected downtime. Furthermore, integrating automatic float switches ensures seamless unattended operation, protecting valuable assets and maintaining continuous site drainage around the clock, even during severe weather emergencies.
Deep Well Water Supply Systems
Accessing clean groundwater requires specialized pumping equipment capable of operating reliably under extreme hydraulic pressure and substantial installation depth. Deep-well and borehole submersible pumps sit submerged far beneath the water table, pushing water upward into pressure tanks, large storage reservoirs, or municipal distribution networks.
This application demands careful engineering calculation and precise hydraulic matching. Operational success relies on balancing the static water level, expected well drawdown, total dynamic head, pipe friction losses, and required discharge pressure at the outlet. Furthermore, motor voltage stability and proper drop cable selection are critical for long-term electrical safety and optimal thermal regulation. Flyaway offers advanced engineering support and robust manufacturing supply chain services to help global clients configure precise well-pump solutions tailored to specific hydrogeological profiles, ensuring continuous water availability for residential communities, commercial facilities, and remote industrial sites.
Agricultural Irrigation and Fluid Transfer
Modern farming, greenhouse management, and landscaping rely heavily on steady, dependable water movement to maximize crop yields. Submersible pumps are widely deployed in agricultural ponds, storage tanks, and large irrigation reservoirs to feed drip lines, center pivot systems, and high-pressure sprinklers efficiently.
Agricultural environments often introduce organic debris such as falling leaves, stringy algae, and fine sediments into the water supply. Protecting the pump inlet with appropriate screening and filtration is essential to prevent blockages during peak irrigation cycles. By utilizing heavy-duty transfer solutions backed by Flyaway manufacturing excellence, agricultural operators secure consistent water pressure across multiple irrigation zones, optimizing crop health while minimizing maintenance overhead. Reliable fluid transfer also plays a critical role in livestock watering, aquaculture management, and fertilizer distribution, making submersible technology an indispensable asset in modern agribusiness operations worldwide.
Wastewater, Sewage, and Lift Stations
Wastewater management requires rugged equipment built specifically for extreme duty cycles and aggressive, unpredictable media. Submersible sewage pumps and lift station units operate in harsh, corrosive environments containing high concentrations of suspended solids, fibrous materials, grease, and aggressive chemicals.
Using a standard clear-water drainage pump in a sewage application invariably leads to immediate mechanical failure and system backup. Municipal and industrial wastewater systems demand specialized vortex, channel, or heavy-duty grinder impellers alongside robust mechanical seals and corrosion-resistant housing. Flyaway delivers comprehensive industrial sewage pumping equipment and reliable supply chain solutions designed to withstand severe municipal and industrial wastewater conditions safely. Proper engineering design in these lift stations prevents environmental contamination, avoids costly emergency repairs, and ensures full compliance with strict municipal sanitation codes.
Key Factors in Submersible Pump Selection
| Operating Parameter | Engineering Consideration | Recommended Flyaway Solution |
| Liquid Type | Clean water vs. abrasive silt vs. raw sewage | Application-matched hydraulic impellers |
| Flow & Head | Calculate vertical lift, friction, and pressure | Customized pump curves and sizing |
| Solids Handling | Screen protection or heavy-duty cutting blades | Clog-free vortex and grinder designs |
| Electrical Setup | Voltage, phase match, cable length, and floats | Robust motor protection and control integration |
Selecting the correct submersible pump prevents costly operational failures, minimizes emergency maintenance, and extends equipment lifespan significantly. Focusing on these engineering fundamentals ensures long-term operational reliability across diverse industrial and municipal sectors. Backed by expert manufacturing capabilities and dependable global supply chain services, Flyaway remains dedicated to providing high-performance fluid handling solutions for every industrial, commercial, and agricultural challenge, ensuring seamless water management wherever it is needed most.